
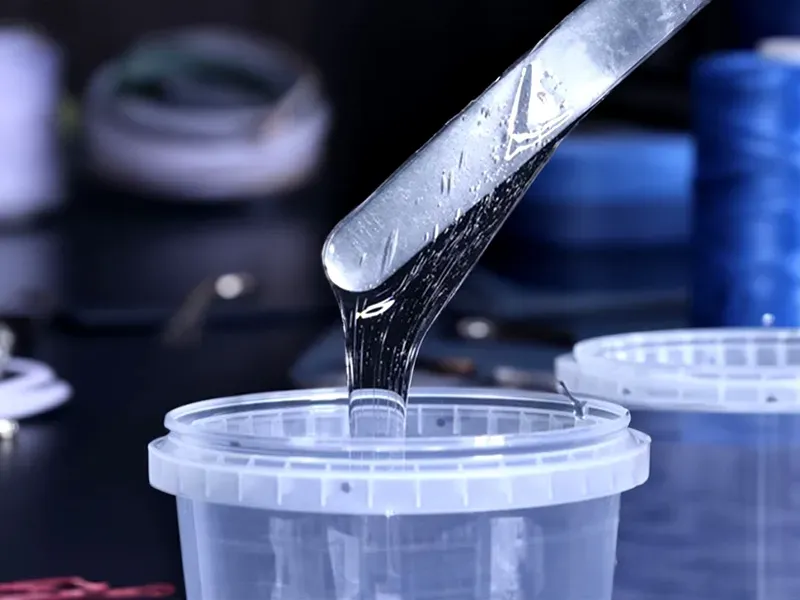
Unlike thermoplastics, LSR flows like water under shear (filling gaps as small as 0.002mm) and undergoes irreversible cross-linking. Choosing a partner who treats LSR like standard resin leads to three silent project killers: uncontrolled scrap, bonding failures, and dimensional instability.
The Unforgiving Nature of LSR: Why Generalist Plastic Molders Fail
Unlike thermoplastics, LSR flows like water under shear (filling gaps as small as 0.002mm) and undergoes irreversible cross-linking. Choosing a partner who treats LSR like standard resin leads to three silent project killers: uncontrolled scrap, bonding failures, and dimensional instability.
The "Flash & Burr" Epidemic
Standard tooling tolerances (±0.02mm) are acceptable for ABS but fatal for LSR. Low viscosity material leaks into every gap.
Heavy flash requires manual trimming, introducing particulate contamination and destroying cleanroom integrity for medical parts.
The Hidden Cost of Runner Waste
Inexperienced molders use simple cold runners or adapted hot runner concepts lacking proper valve gates.
Material waste can exceed 40% of shot weight. Since medical LSR costs 5x-10x more than resin, this effectively doubles your BOM cost.
The Interface Failure (Overmolding)
Mismatched thermal expansion between metal inserts and silicone, or improper chemical priming.
Delamination and leakage. The bond fails under stress, leading to massive field recalls of “waterproof” devices.
Don't let manufacturing risks derail your project. You don't just need a supplier who can run a machine; you need an engineering partner who masters the complex science of precision LSR Injection Molding.
Why Choose UsThe LSR Ecosystem: Vertically Integrated Manufacturing
We bridge the gap between Material Science and Cleanroom Mass Production. Our unified "Under One Roof" workflow eliminates tolerance stack-up and accelerates validation.
01 Material Engineering
Expert sourcing from top-tier vendors like Wacker, Dow, and Shin-Etsu to ensure unbiased material performance. We provide custom color matching and biocompatibility verification across a wide durometer range (10-80 Shore A) tailored to your application.
02 Cold Deck Tooling
In-house precision tooling specializing in high-efficiency, flashless LSR molds. Utilizing Stavax/S136 steel and advanced valve-gated systems, we eliminate material waste and ensure perfect part-to-part consistency.
03 Cleanroom Molding
Contamination-free production within ISO Class 8 cleanroom injection cells. Our fully automated workflow features closed-loop dosing and robotic demolding to guarantee zero human contact and medical-grade purity.
04 Post-Curing & Finish
Validated post-curing processes (4 hours @ 200°C) to drive out volatiles and ensure full regulatory compliance. We utilize cryogenic deflashing to deliver high-precision components with superior dimensional stability and edge quality.
Engineered Material Selection & Precision Manufacturing Specs
Data-Driven Manufacturing: We validate material properties against your functional requirements, ensuring optimal Shore A hardness, elongation, and tear strength.
| Material & Finish Matrix | Classification | Primary Characteristics | Secondary Specifications | Key Features & Ideal Applications |
|---|---|---|---|---|
| Standard LSR | General Purpose | Hardness: 20-80 Shore A | Temperature: -50°C to 200°C | Best for industrial gaskets, keypads, and grommets. Offers excellent mechanical resilience. |
| Medical Grade LSR | USP Class VI | Compliance: ISO 10993 Biocompatible | Purity: Platinum Cured System | Ideal for life-saving catheters, valves, and surgical seals. Highly sterile and non-reactive. |
| Optical Grade LSR | Optical / Transparent | Clarity: >94% Light Transmission | Feature: Non-Yellowing UV Resistant | Engineered for LED lenses and light guides. Superior alternative to polycarbonate or glass. |
| Fluorosilicone (F-LSR) | Harsh Environment | Resistance: Fuels, Oils & Solvents | Base Chemistry: Fluorocarbon | Crucial for automotive fuel systems and aerospace seals exposed to aggressive chemicals. |
| SPI-A2 (Diamond Buff) | High Gloss Finish | Function: Maximum Optical Clarity | Attribute: High Friction (Tacky surface) | Essential for clear lenses. Creates a highly hygienic, smooth, bacteria-resistant surface. |
| PM-T1 (Bead Blast) | Matte Texture | Function: Low Friction / Anti-Tack | Attribute: Non-reflective | Provides a premium "Soft Touch" ergonomic feel. Prevents part sticking and hides fingerprints. |
Material Decision Framework
Don't let material selection define your failure. Understand the trade-offs between LSR, HCR, and TPE.
| Performance Feature | LSR (Liquid Silicone) | HCR (Solid Gum) | TPE (Thermoplastic) |
|---|---|---|---|
| Process Methodology | Fully Automated Injection | Manual Compression/Transfer | High-Speed Automated Injection |
| Cycle Time Efficiency | Fast (Seconds) | Slow (Minutes) | Ultra-Fast (Seconds) |
| Thermal Resistance | Excellent (Up to 250°C) | Excellent (Up to 250°C) | Limited (Melts >100°C) |
| Compression Set | Very Low (Superior Sealing) | Low (Stable Performance) | High (Susceptible to Leaks) |
| Precision Tolerances | ±0.08mm (High Accuracy) | ±0.25mm (Standard) | ±0.10mm (Moderate) |
| Min. Wall Thickness | 0.20 mm (Thin-Wall Capable) | 0.80 mm (Limited Flow) | 0.50 mm (Standard) |
| Cleanroom Capability | ISO Class 8 (100k) Available | Standard Industrial | Standard Industrial |
| Biocompatibility | Superior (ISO 10993/USP VI) | Good (Medical Grades Exist) | Variable (Application Specific) |
| Chemical Resistance | High (Non-reactive) | High (Non-reactive) | Moderate (Solvent Sensitive) |
| Unit Cost @ Volume | Lowest (>100k Units) | High (Labor Intensive) | Low (Efficient Production) |
| Ideal Use Case | Complex Medical & Optical | Low-Volume Heavy Industrial | Consumer Goods & Recycling |
Applied Manufacturing & Technical Validation
Review our documented production records across injection molding and metal component integration. Examine how we resolve complex geometric challenges and strictly control critical dimensions to ensure structural and functional reliability in demanding environments.
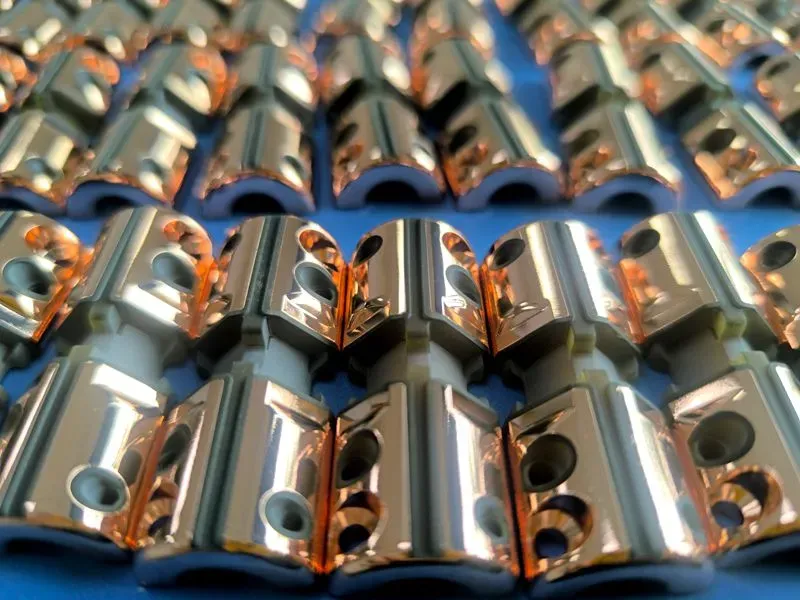
Overcoming RF Leakage: Engineering Zero-Gap Balun Assemblies for MRI Diagnostics
Client Type Leading Tier-1 Medical Imaging OEMProduction Volume 15,000+ units/yearMaterial Used Unfilled Polyetherimide (PEI)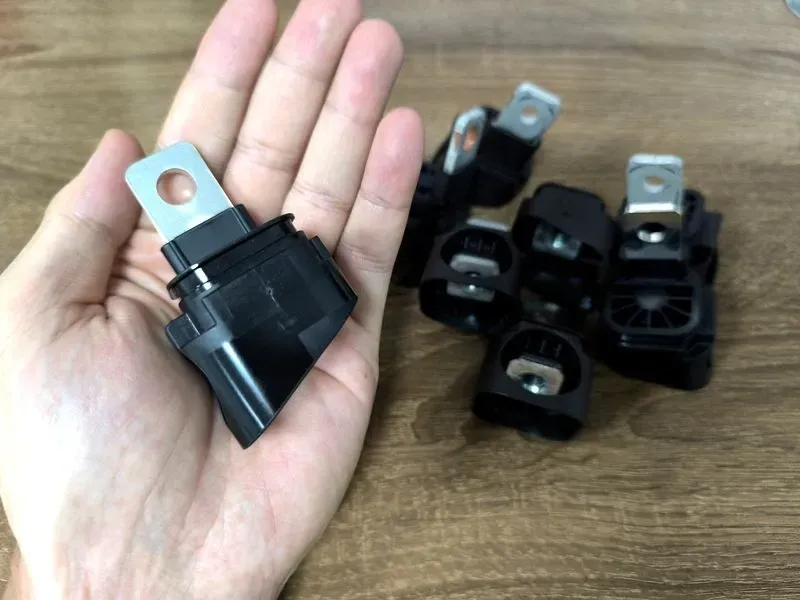
Overcoming CTE Mismatch: Engineering 800V Busbar Terminals for Commercial EVs
Client Type Leading Heavy-Duty Commercial EV Manufacturer - Tier 1Production Volume 250,000+ units/yearMaterial Used High-Purity C11000 Copper & PA6 GF30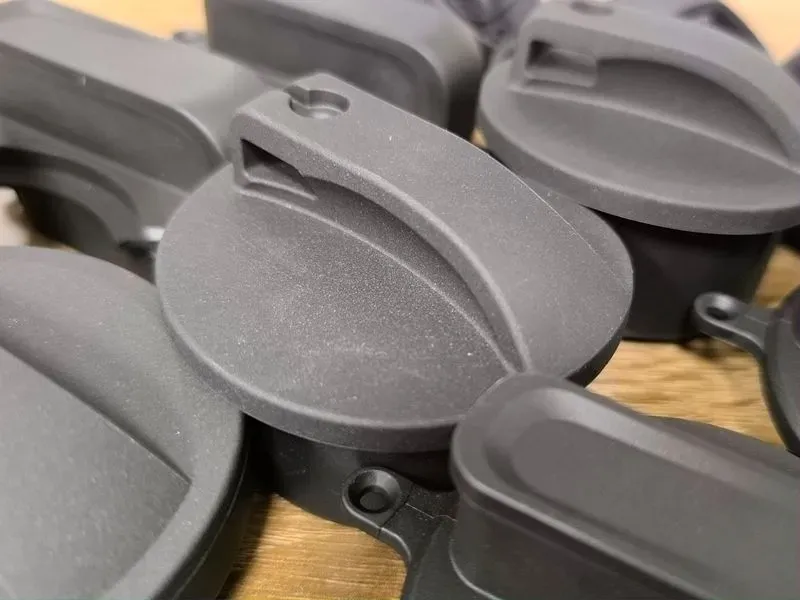
Solving Material Fatigue: Engineering a Monolithic FR-TPU Dust Cover for NEV Platforms
Client Type Leading Chinese NEV Manufacturer (Tier 1)Production Volume 500,000+ units/yearMaterial Used Custom Polyether-based FR-TPU (UL94 V-0)Request DFM EvaluationSee More Case StudiesRESIN CAPABILITIESDeploy Advanced Multi-Material Injection Molding Capabilities
PC ABS Injection Molding
Expert PC/ABS injection molding services combining polycarbonate toughness with ABS processability. We specialize in stress-free, high-impact parts for automotive interiors, thin-wall electronics, and chrome-plating applications, featuring IATF 16949 certified scientific molding and zero-flash metal insert integration.
Learn More
Delrin® Injection Molding
Expert custom Delrin® (POM) injection molding. We master 2-3% shrinkage with IATF 16949 certified quality to deliver void-free, tight-tolerance precision parts.
Learn More
LDPE Injection Molding
Expert LDPE injection molding delivering defect-free soft plastics. Featuring 64+ cavity high-volume scalability and advanced cooling for zero warpage.
Learn More
PEEK Injection Molding
High-performance PEEK molding for mission-critical components in extreme environments. Engineering-led precision with full material traceability.
Learn MoreRequest DFM EvaluationExplore More Molding ServicesTECHNICAL REFERENCEFrequently Asked Questions
Answers to common questions regarding precision, tooling, materials, and our integrated molding capabilities.
Still have questions?
Our engineering team loves solving complex problems. Chat with us or send your drawing for a review.
Request DFM EvaluationReady to Manufacture With One Accountable Factory?
From in-house tooling to high-volume production — stamping, molding, plating and assembly under one IATF 16949 roof. Send your spec and volume, get a quote within 24 hours.