
Advanced ABS Injection Molding: Engineered for High-Impact Dimensional Stability
Mastering ABS material science, we optimize injection rheology and thermal control to eliminate typical defects like environmental stress cracking in demanding industrial applications. Utilizing advanced techniques such as RHCM for high-gloss, weld-line-free finishes, our IATF 16949 compliant proce…
Mastering ABS material science, we optimize injection rheology and thermal control to eliminate typical defects like environmental stress cracking in demanding industrial applications. Utilizing advanced techniques such as RHCM for high-gloss, weld-line-free finishes, our IATF 16949 compliant process guarantees dimensional consistency and flawless structural integrity across high-volume production runs.
Precision Molding: 50T-1200T ABS capacity.Insert Molding: Induction pre-heated metal contacts.RHCM Tech: High-gloss piano black finish.Turnkey Assembly: Ultrasonic welding and packaging.Request DFM EvaluationSee Material Database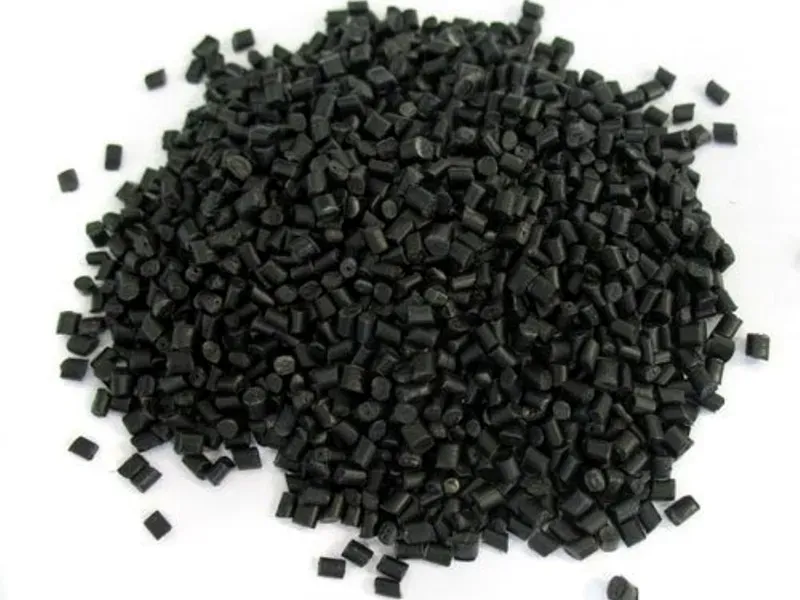
The Invisible Risks in Custom ABS Molding: Why Designs Fail in Production
ABS is the workhorse of the plastics industry, but it is unforgiving. Without rigorous process control and DFM, hidden defects can compromise your product's integrity and delay your launch.
The "Cosmetic Nightmare"
High-gloss ABS reveals every imperfection. Improper gating or venting leads to visible weld lines, while insufficient drying causes “splay marks,” making premium products look cheap.
Consequence: High rejection rates & brand damage.
The "Silent Killer" (ESC)
Molding ABS around cold metal inserts creates locked-in stress. Exposure to cleaning solvents can trigger spontaneous cracking weeks after assembly.
Consequence: Catastrophic field failures & recalls.
The "Assembly Deadlock"
Sourcing plastic and metal from different vendors leads to tolerance stack-up. The plastic shrinks, the metal springs back, and components fail to mate.
Consequence: Production halts & endless finger-pointing.
Don't let manufacturing risks derail your project. You don't just need a supplier who can run a machine; you need an engineering partner who masters the complex science of precision ABS Injection Molding.
Why Choose UsOur 4 Engineering Pillars: Redefining Custom ABS Manufacturing
We don’t just mold parts; we engineer solutions. Our integrated approach bridges the critical gap between design concepts and mass production reality.
Integrated ABS & Metal Solutions
Most molders outsource metal hardware, leading to tolerance issues. We manufacture precision terminals and brackets in-house, ensuring a hermetic bond between the insert and ABS flow.
ABS Material Science
From UL94 V-0 for electronics to Plating Grade for automotive. We help you choose between premium global resins (Sabic) or cost-effective Asian equivalents (Chi Mei) to match specs and budget.
Scientific Molding & DFM
Using Moldflow simulation, we decouple filling, packing, and holding phases. This rigorous control eliminates sinks, warpage, and internal stress, guaranteeing dimensional consistency.
Factory-Direct Access
Bypass the sales clerks. You get direct access to our project managers and tooling engineers. We provide transparent BOM breakdowns, video audits, and clear mold modification logs.
ABS Material Engineering: From General Purpose to High-Performance
ABS is not a “one-size-fits-all” resin. We help you navigate the material spectrum to balance impact resistance, heat deflection, and aesthetic finish.
| ABS Grade & Category | Typical Specs / Materials | Key Characteristics & Engineering Benefits | Primary Industry Applications |
|---|---|---|---|
| General Purpose & High Gloss | e.g., Polylac PA-757 | Optimized for Class-A "Piano Black" finishes without secondary painting. Offers a superior balance of impact resistance, rigidity, and high flow for complex molds. | Consumer electronics housings, smart home devices, cosmetic bezels, and everyday appliances. |
| Flame Retardant (FR) | UL94 V-0 / 5VB | Engineered to resist ignition and prevent flame spread. Rigorously processed to ensure RoHS compliance while mitigating material degradation risks during injection molding. | Power electronics, router housings, battery enclosures, and industrial control panels. |
| Plating & High-Heat | Automotive Trim Grade | Formulated for excellent electroplating properties (superior chrome adhesion) and elevated Heat Deflection Temperature (HDT) to endure severe environmental thermal cycling. | Automotive interior and exterior trim, plated radiator grilles, and decorative mobility bezels. |
| Glass-Fiber Reinforced | 10% - 30% GF | A reinforced structural matrix that dramatically increases tensile strength, enhances stiffness, lowers shrinkage rates, and provides excellent long-term dimensional stability. | Internal structural brackets, precision gears, mechanical housings, and load-bearing chassis. |
| Medical Grade (Bio-compatible) | ISO 10993 / USP Class VI | Demonstrates exceptional resistance to Environmental Stress Cracking (ESC) and degradation from harsh hospital-grade chemical disinfectants and sterilization processes. | Handheld diagnostic scanners, patient monitors, and non-invasive medical lab equipment. |
| PC/ABS Alloy | High-Impact Blend | Combines the superior processability of ABS with the extreme mechanical toughness and heat resistance of Polycarbonate. Excellent for parts requiring snap-fit assemblies. | Automotive HVAC vents, structural crash components, and ruggedized electronic enclosures. |
ABS Design Guide & DFM Cheat Sheet
Don't wait for the T1 trial to find errors. Follow these critical design rules to ensure your ABS parts are moldable, cost-effective, and defect-free.
| Design Element (CAD) | Recommended Parameters | Engineering Rationale & Impact |
|---|---|---|
| Wall Thickness (Uniformity) | Maintain nominal walls between 1.5mm - 3.5mm. | Strict uniformity is critical to prevent differential cooling rates, which are the primary cause of part warpage, internal stress, and dimensional instability. |
| Draft Angles | Min 0.5° for polished surfaces. Add 1.0° - 1.5° per 0.025mm depth for textured finishes (MT/VDI). | Ensures smooth and rapid part ejection from the mold cavity, preventing cosmetic scuff marks, drag lines, and mechanical stress on the ejection pins. |
| Rib Design (Ratio) | Rib base thickness should strictly be 50% - 60% of the adjacent wall thickness. | Mitigates the risk of thermal mass accumulation, thereby preventing unsightly sink marks on the cosmetic A-Surface while maintaining structural rigidity. |
| Corner Radii | Avoid sharp corners. Apply a minimum internal radius of 0.5mm. | Reduces high stress concentration points that lead to premature mechanical failure, and promotes smooth, uniform molten resin flow during the injection phase. |
Applied Manufacturing & Technical Validation
Review our documented production records across injection molding and metal component integration. Examine how we resolve complex geometric challenges and strictly control critical dimensions to ensure structural and functional reliability in demanding environments.
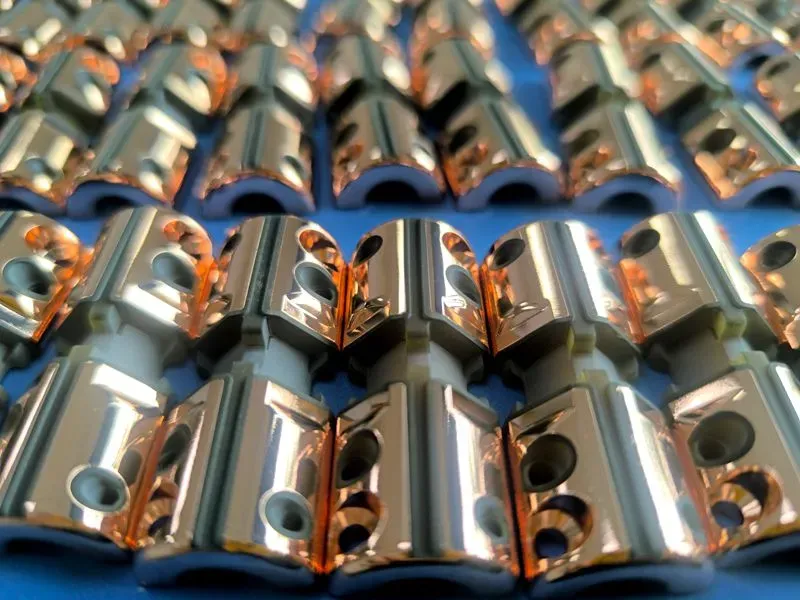
Overcoming RF Leakage: Engineering Zero-Gap Balun Assemblies for MRI Diagnostics
Client Type Leading Tier-1 Medical Imaging OEMProduction Volume 15,000+ units/yearMaterial Used Unfilled Polyetherimide (PEI)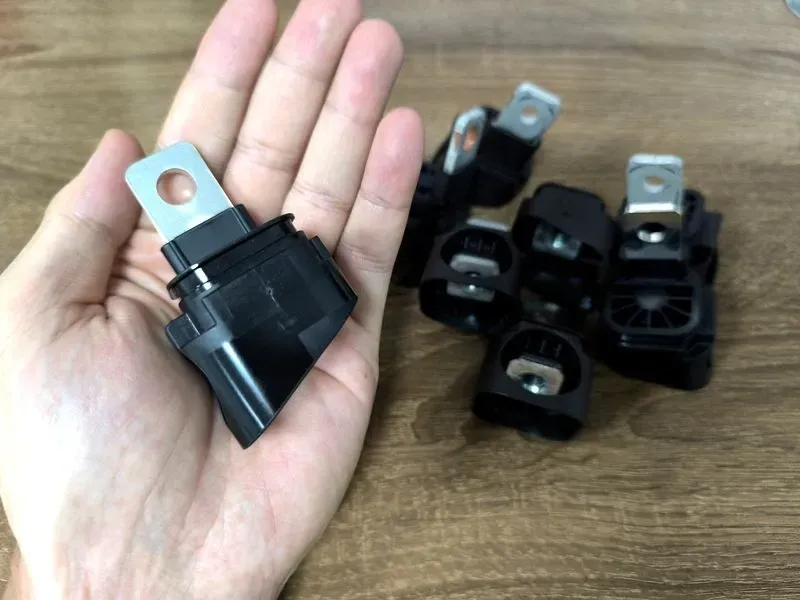
Overcoming CTE Mismatch: Engineering 800V Busbar Terminals for Commercial EVs
Client Type Leading Heavy-Duty Commercial EV Manufacturer - Tier 1Production Volume 250,000+ units/yearMaterial Used High-Purity C11000 Copper & PA6 GF30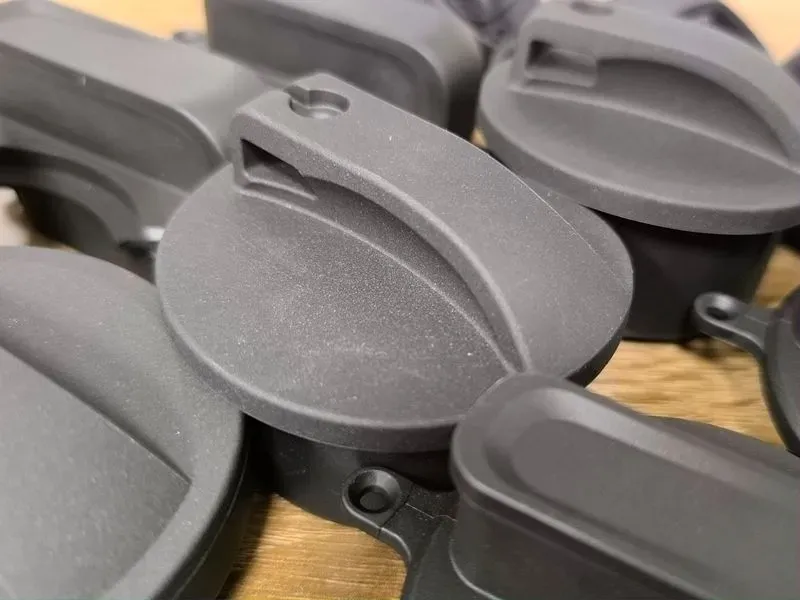
Solving Material Fatigue: Engineering a Monolithic FR-TPU Dust Cover for NEV Platforms
Client Type Leading Chinese NEV Manufacturer (Tier 1)Production Volume 500,000+ units/yearMaterial Used Custom Polyether-based FR-TPU (UL94 V-0)Request DFM EvaluationSee More Case StudiesRESIN CAPABILITIESDeploy Advanced Multi-Material Injection Molding Capabilities
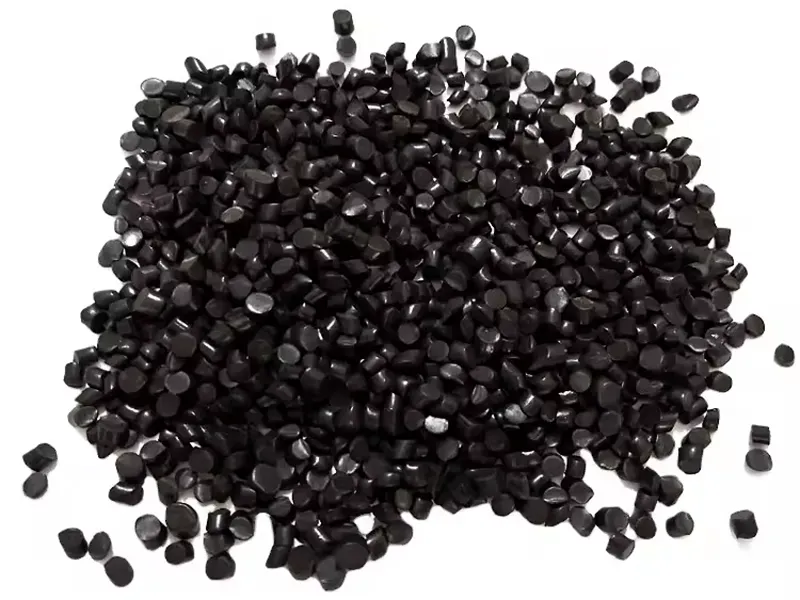
HDPE Injection Molding
Precision HDPE molding mastering 3% shrinkage and environmental stress cracking. Equipped with 50T to 1,200T capacity and in-house metal insert hybrid molding.
Learn More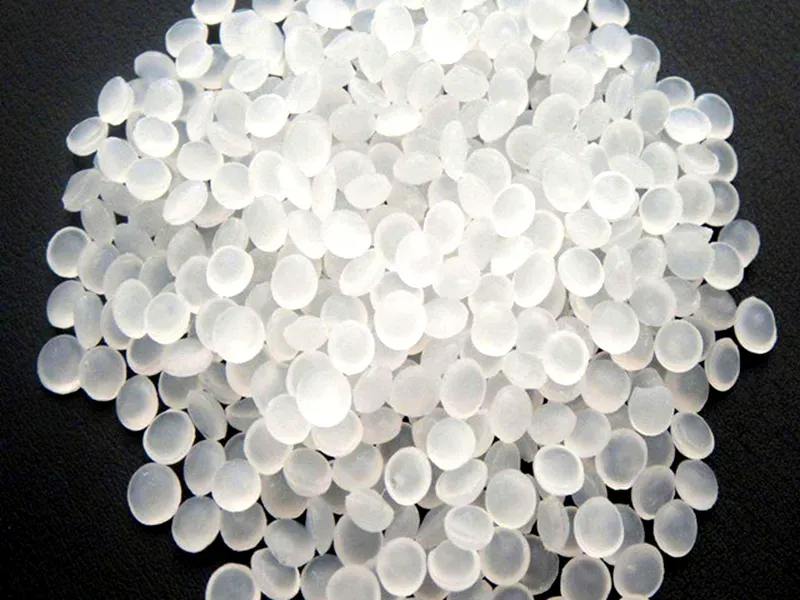
PP Injection Molding
IATF 16949 certified PP injection molding controlling aggressive shrinkage. From durable living hinges to high-volume 800T automotive components.
Learn More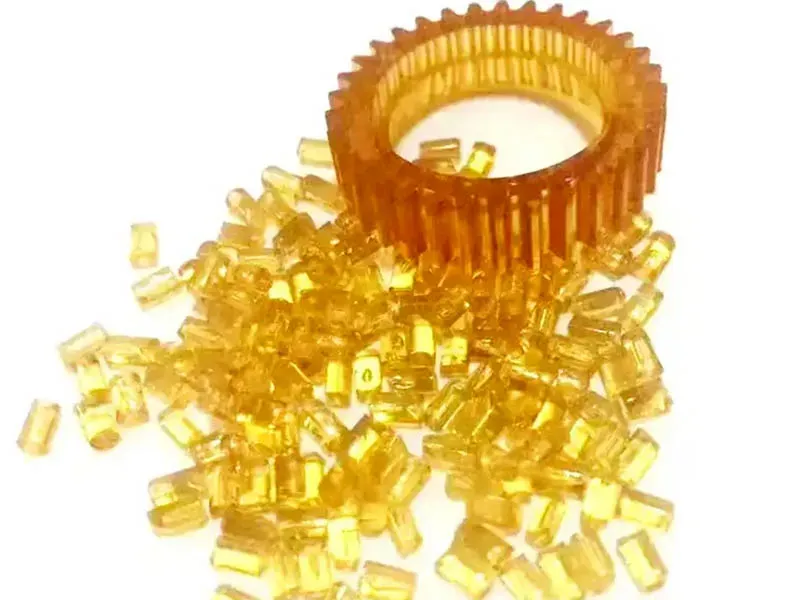
PEI Injection Molding
Expert PEI (Ultem™) injection molding for mission-critical applications. Mastering high-heat processing and CTE mismatch for aerospace, medical, and EV sectors.
Learn More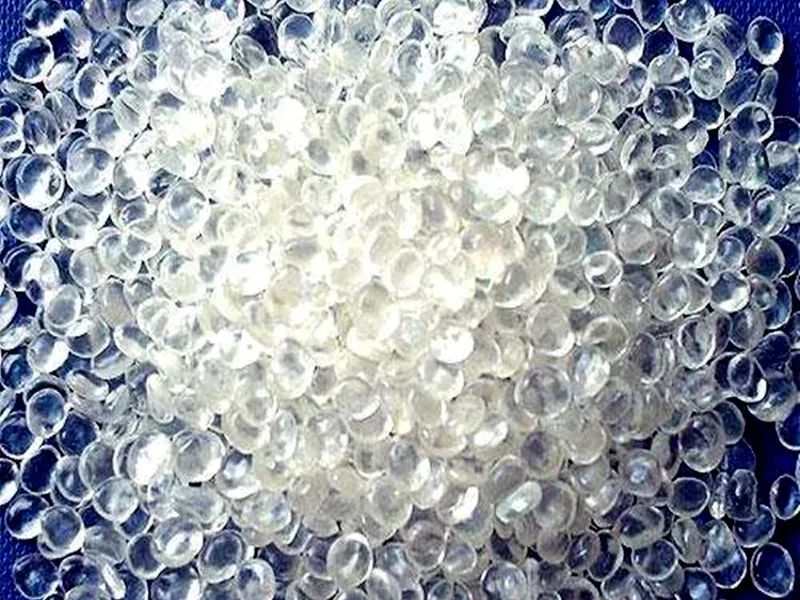
TPU Injection Molding
Master of TPU injection and overmolding. Utilizing 30+ specialized machines to deliver high-precision, defect-free elastomer components.
Learn MoreRequest DFM EvaluationExplore More Molding ServicesTECHNICAL REFERENCEFrequently Asked Questions
Answers to common questions regarding precision, tooling, materials, and our integrated molding capabilities.You retain 100% ownership. We provide a formal Mold Ownership Certificate and store your tools in our climate-controlled vault for free. You can transfer them to another supplier at any time.
We eliminate internal stress during insert molding by using induction pre-heating stations. This ensures the metal terminals match the ABS temperature, preventing catastrophic field failures and extending product lifespan.
Yes, we utilize Rapid Heat Cycle Molding (RHCM) technology to produce high-gloss, Class-A surfaces. This process fuses weld lines completely, eliminating the need for secondary painting and significantly reducing your unit costs.
We implement structural savings like Yudo Hot Runners to reduce material waste and conformal cooling to cut cycle times by up to 30%. We also offer strategic material substitution using Tier-1 Asian equivalents to lower resin costs by up to 25% while maintaining UL listings.
Standard T1 samples take 15 to 25 calendar days. While our typical MOQ is 1,000 units, we support low-volume bridge tooling and pilot runs starting at 500 units to help you launch successfully.
Yes, to prevent tolerance mismatches, we manufacture precision terminals and brackets in-house. This guarantees a perfect hermetic bond between the metal insert and the plastic, giving us single-source responsibility for the final fit.
Absolutely. Beyond molding, we handle ultrasonic welding, thermal heat staking, and mechanical assembly. We can install PCBs, apply retail packaging, and ship ready-to-sell units directly to your dock.
We are IATF 16949 and ISO 9001 certified. Our process relies on scientific molding, Moldflow simulation, and rigorous IPQC patrol inspections using CMM metrology to ensure every part matches the golden sample.

Still have questions?
Our engineering team loves solving complex problems. Chat with us or send your drawing for a review.
Request DFM EvaluationReady to Manufacture With One Accountable Factory?
From in-house tooling to high-volume production — stamping, molding, plating and assembly under one IATF 16949 roof. Send your spec and volume, get a quote within 24 hours.